Skip to content
The MBR STP Monitoring System aimed to modernize sewage treatment operations by implementing a centralized smart monitoring and predictive maintenance platform. The objective was to improve real-time visibility of the Membrane Bioreactor process, enhance treatment efficiency, maintain consistent membrane performance, minimize operational issues, optimize equipment maintenance schedules, reduce unexpected downtime, improve energy efficiency, and ensure reliable operation across residential, commercial, industrial, and municipal sewage treatment facilities.
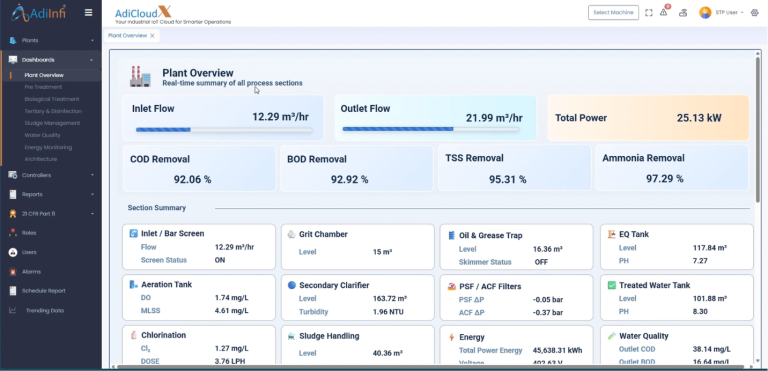
By integrating the IoT-based cloud platform AdiCloudX with the AdiNexus Industrial IoT Gateway, the entire MBR STP infrastructure was transformed into a digitally connected and intelligent monitoring system. The solution enabled real-time monitoring of critical treatment parameters, including inlet and outlet flow, water levels, MBR cycle status, membrane filtration process, transmembrane pressure (TMP), aeration process, blower operation, feed and circulation pump status, permeate pump operation, valve operation, dissolved oxygen levels, pH, turbidity, membrane health, motor health, sludge handling systems, power consumption, controller status, communication systems, emergency alarms, fault conditions, and other critical operational parameters through a centralized dashboard accessible from anywhere.
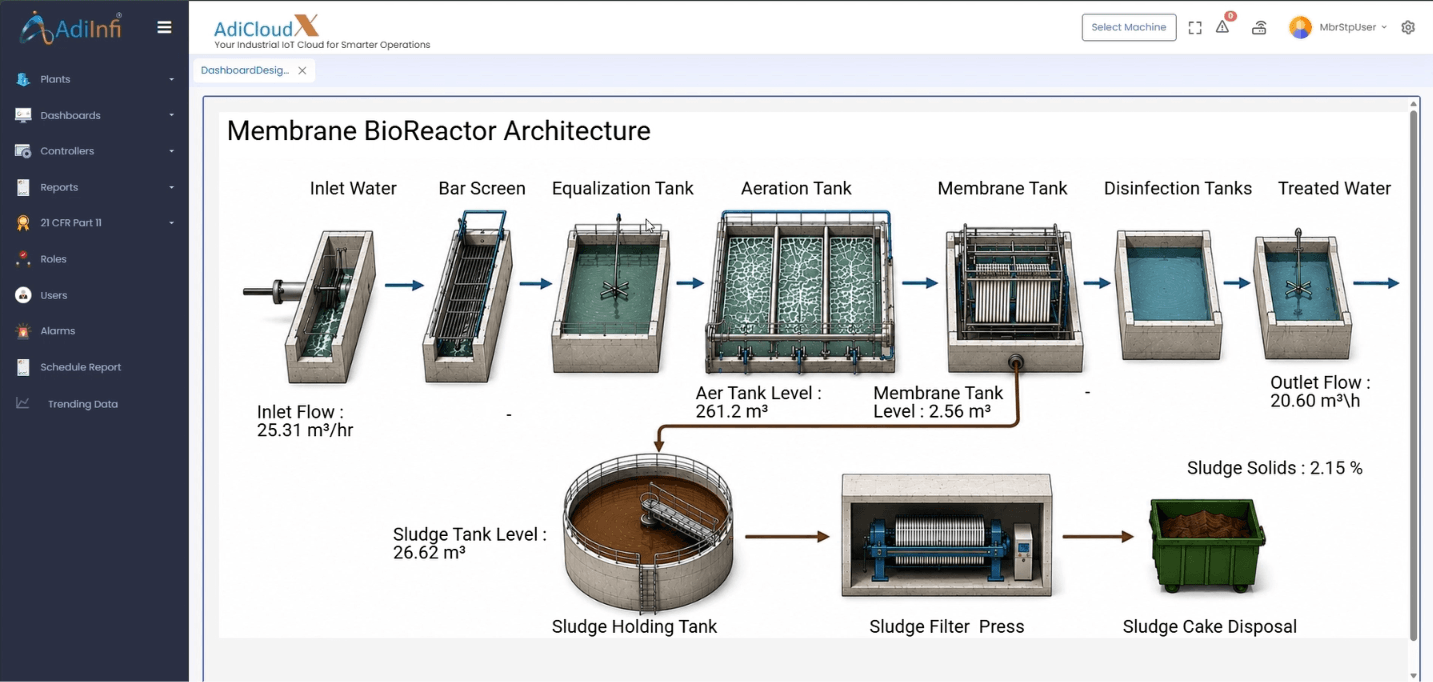
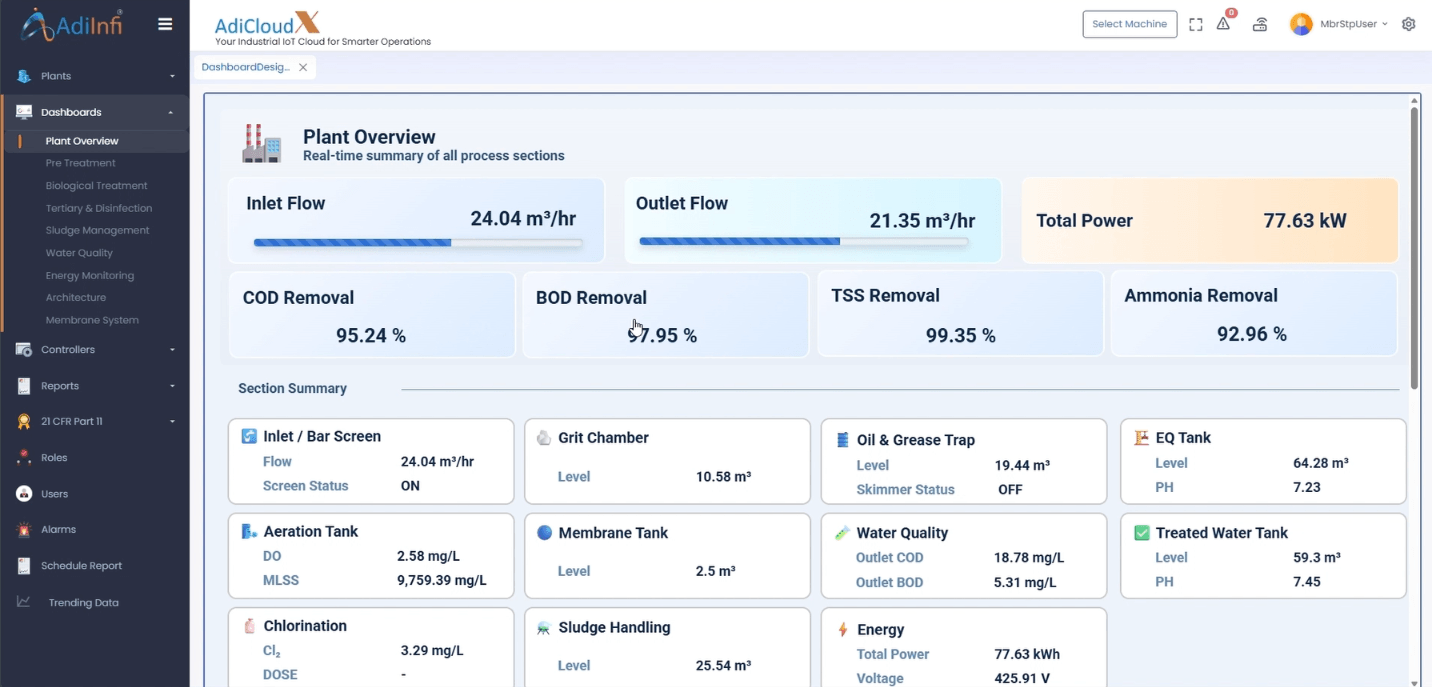
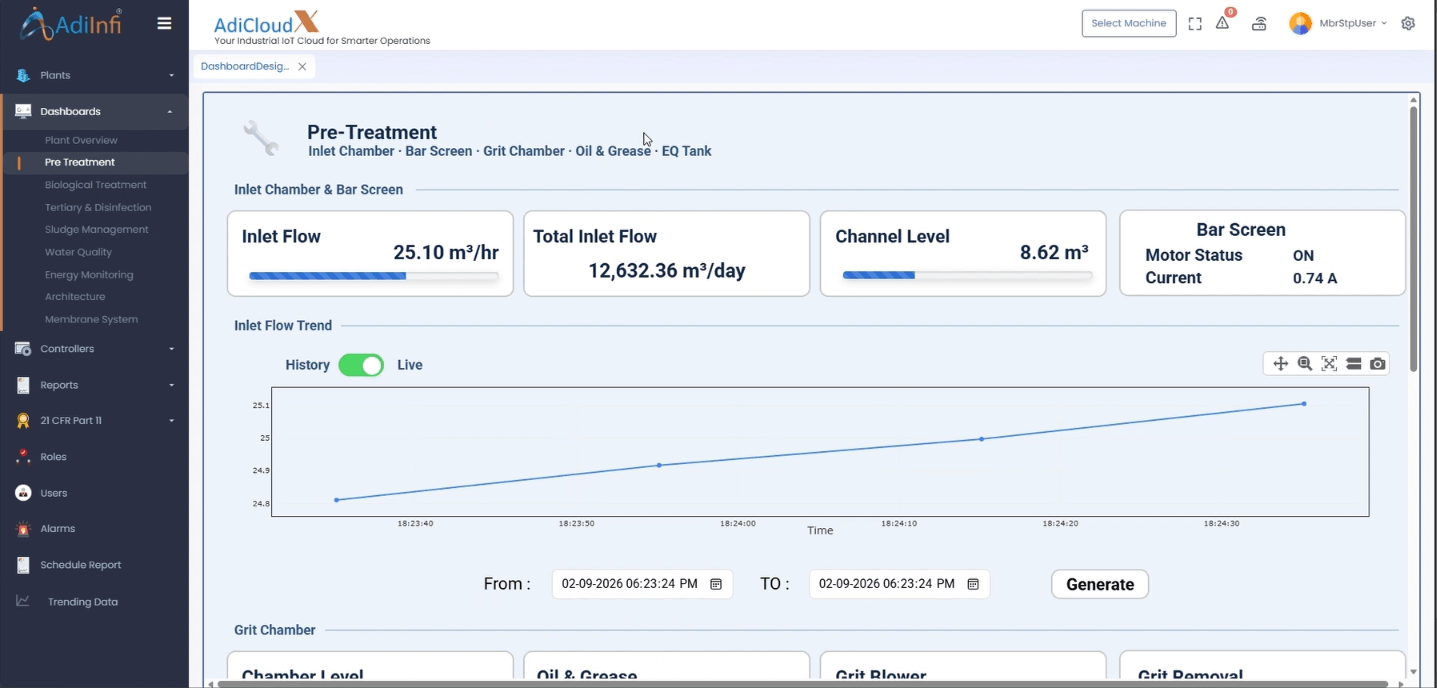
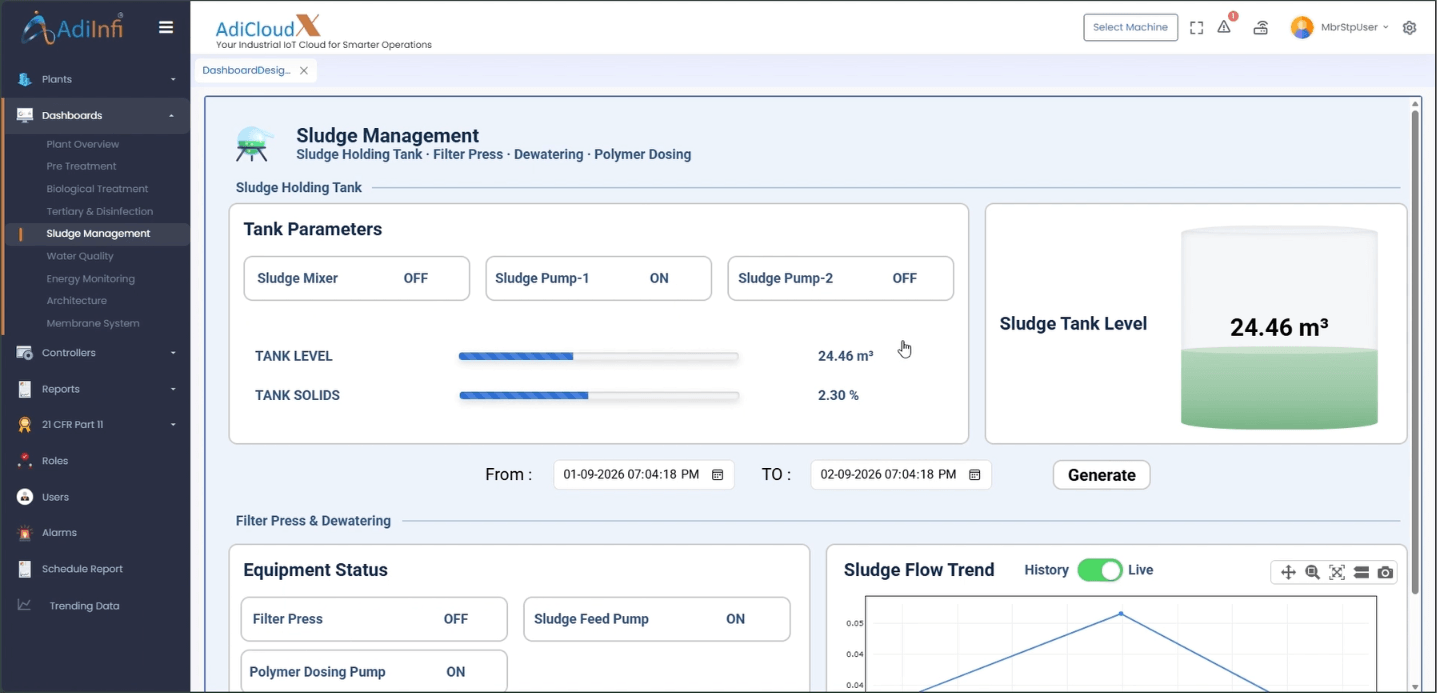
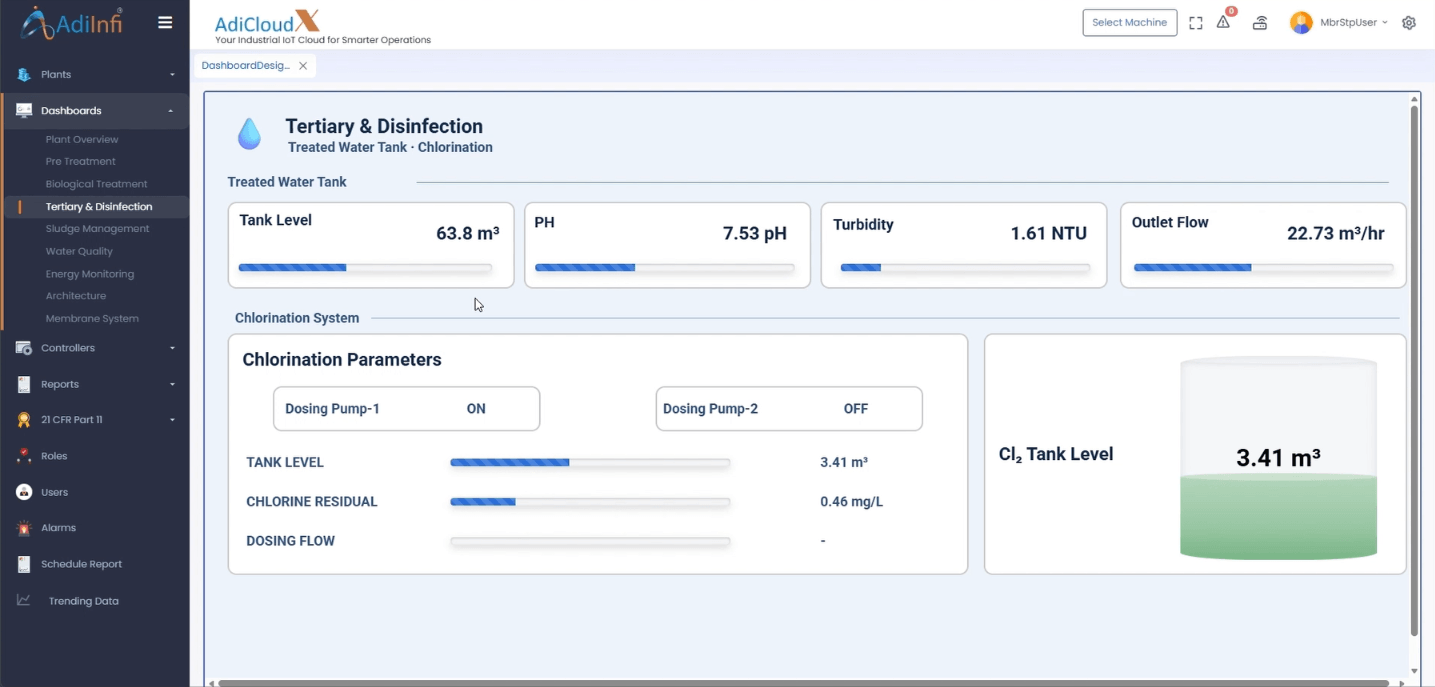
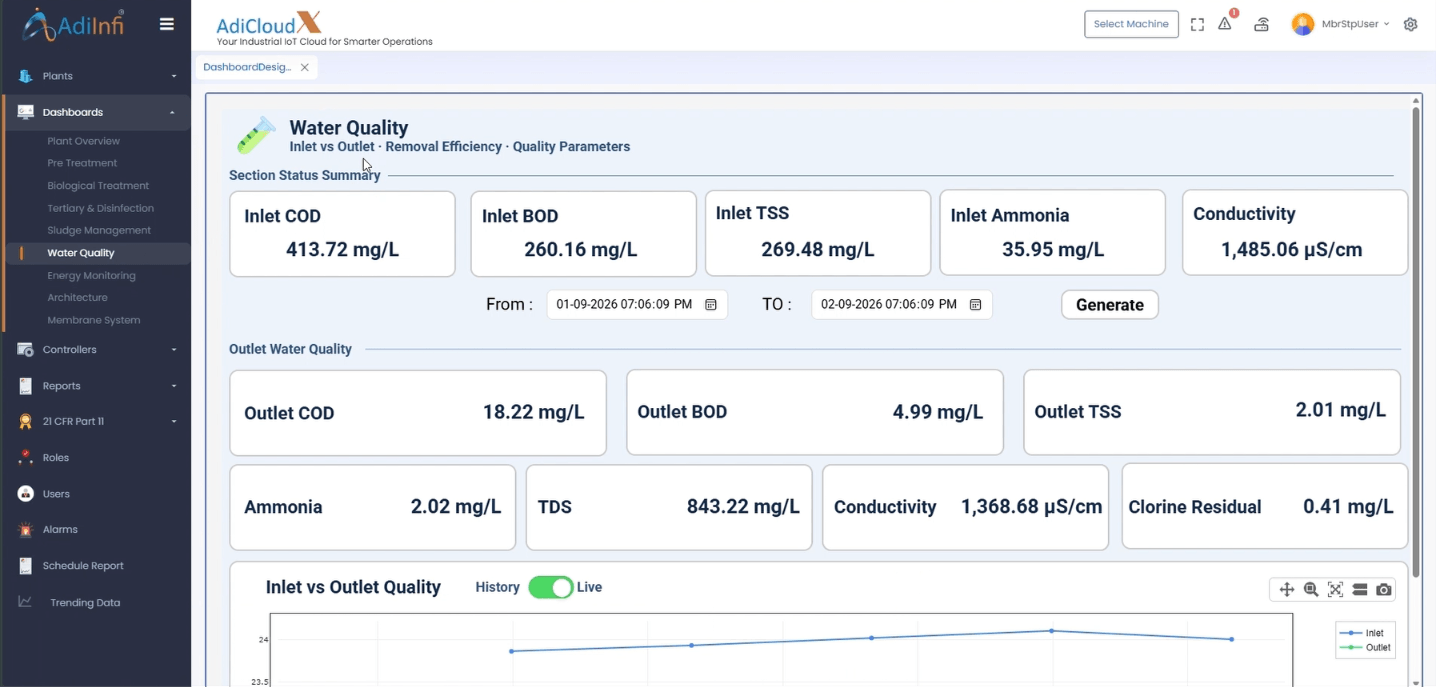
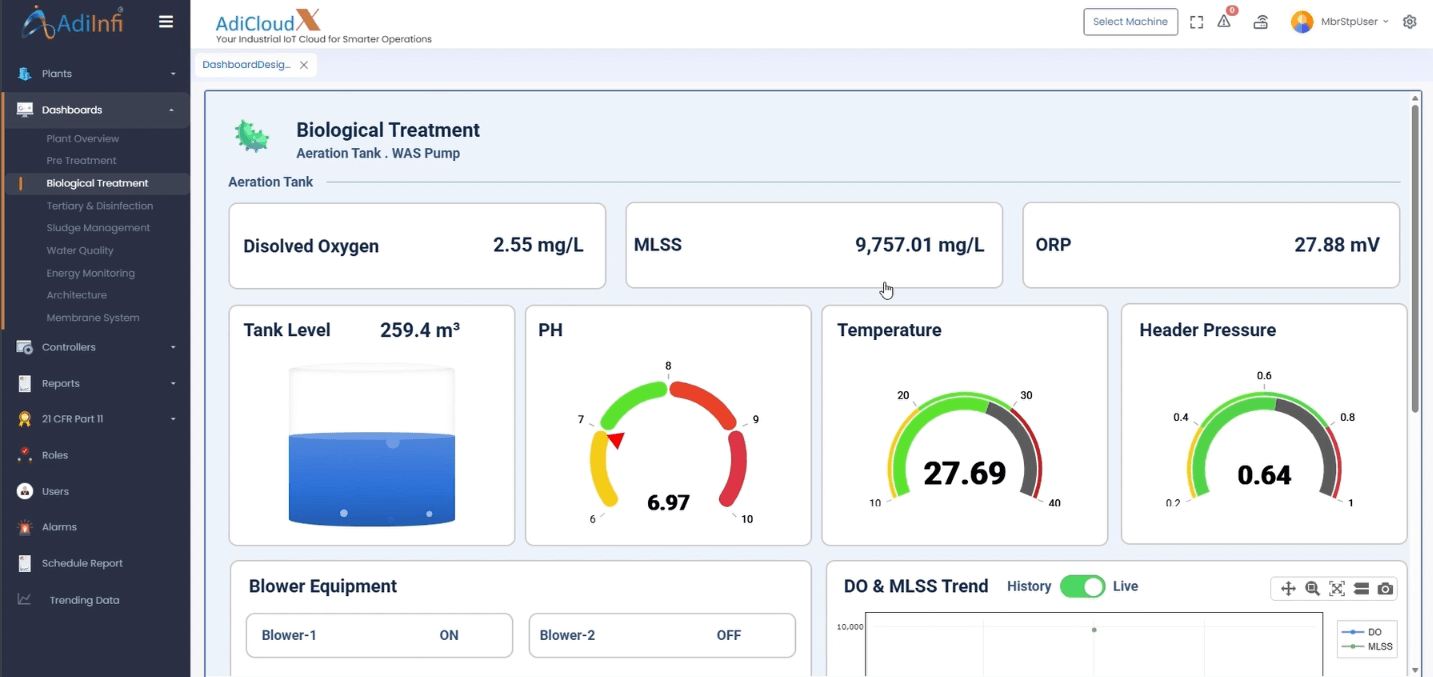
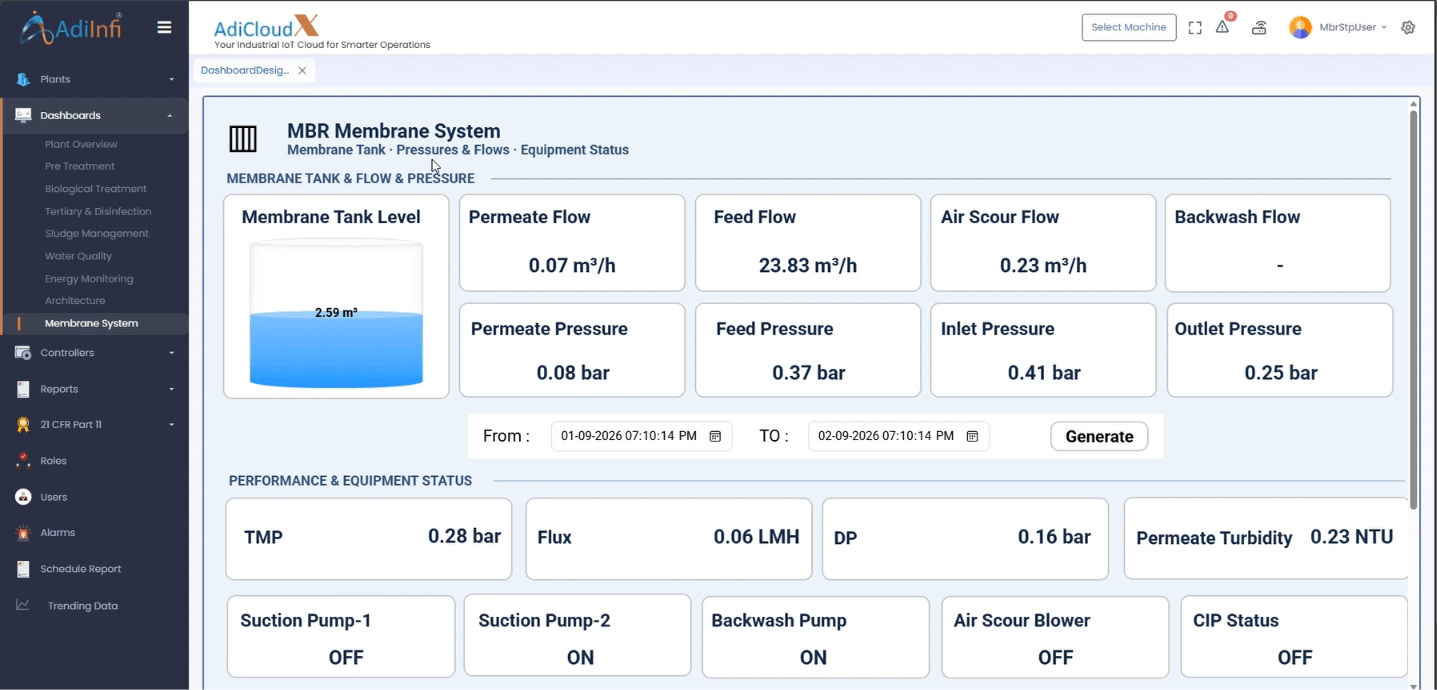
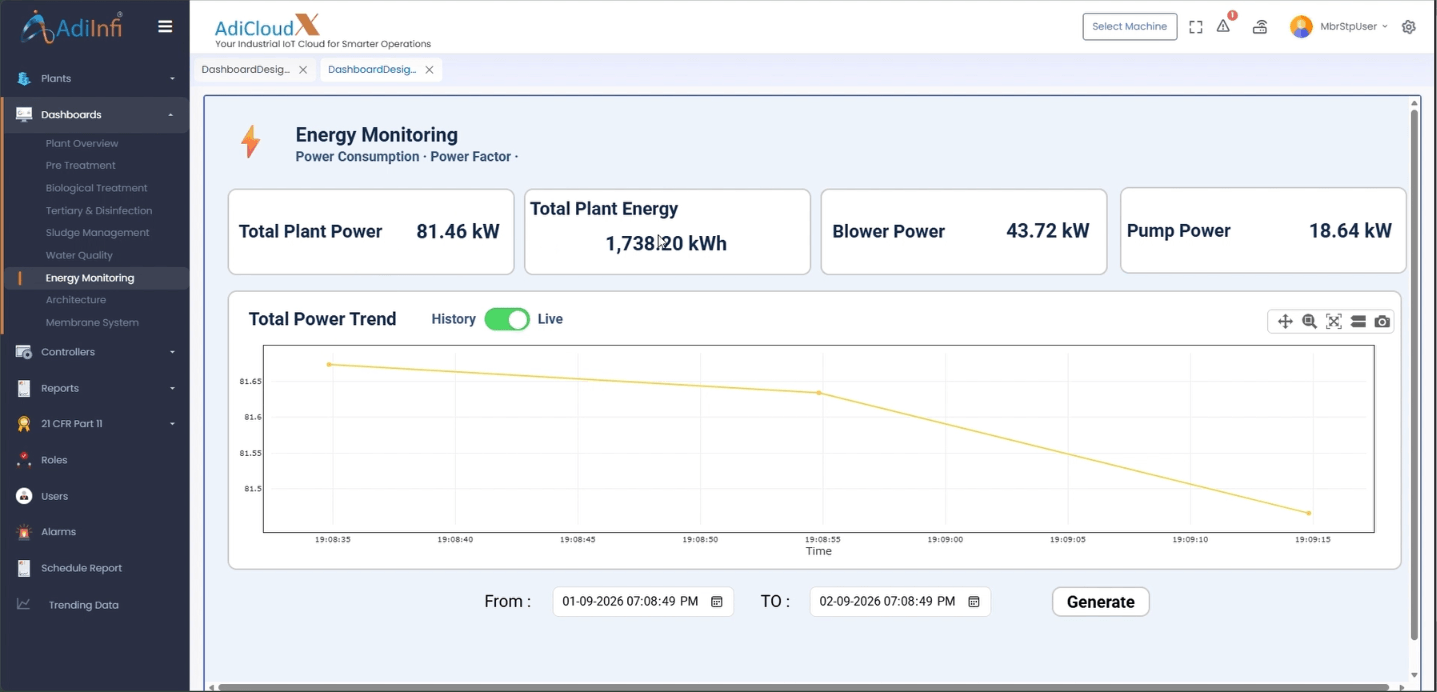
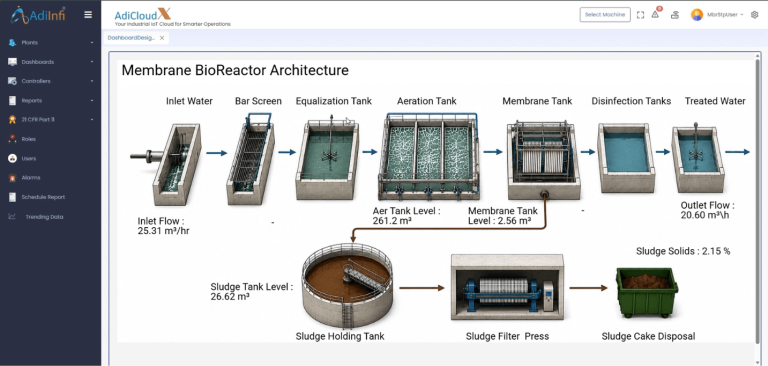
MBR STP Monitoring System Overview
The implementation focused on building a scalable, secure, and intelligent SCADA platform for centralized monitoring and management of MBR sewage treatment plant operations. The solution provides real-time visibility into the membrane treatment process, improves operational efficiency, reduces equipment downtime, and supports proactive maintenance through a unified dashboard.
MBR Process Monitoring
- Monitors MBR tank levels, filtration status, aeration, membrane operation, permeate flow, and sludge handling processes
- Tracks each stage of the MBR treatment process and operational sequence in real time
- Provides centralized visualization of critical sewage treatment and membrane filtration activities
Water Quality & Process Monitoring
- Monitors key process parameters such as dissolved oxygen, pH, flow, turbidity, and membrane operating conditions
- Tracks membrane pressure and transmembrane pressure (TMP) to identify abnormal filtration conditions
- Helps maintain consistent treatment performance and improve overall process efficiency
Equipment & Motor Health
- Tracks the performance of feed pumps, permeate pumps, blowers, circulation pumps, motors, valves, and other critical equipment
- Monitors operating status, motor health, membrane operation, and abnormal equipment conditions
- Supports proactive maintenance to minimize unexpected downtime and maintain reliable plant operation
Power & Fault Monitoring
- Monitors power supply, voltage, current, energy consumption, and equipment fault conditions
- Detects electrical abnormalities, equipment failures, membrane-related issues, and operational faults in real time
- Improves plant reliability, energy efficiency, and maintenance effectiveness
Challenges Before AdiCloudX Implementation
Before adopting AdiCloudX, sewage treatment plant operators faced several operational and maintenance challenges that impacted treatment efficiency, membrane performance, equipment reliability, energy consumption, and overall plant performance.
Manual Monitoring & Plant Operation
- MBR process stages and equipment conditions were monitored manually
- Delayed identification of process abnormalities, membrane issues, and increased operator effort
- Limited historical records for treatment, membrane, and equipment performance analysis
Limited Real-Time Visibility
- No centralized dashboard to monitor MBR process status, tank levels, membrane filtration, pumps, blowers, valves, and process parameters
- Difficult to track multiple treatment units and critical equipment from a single location
Equipment Failures & Downtime
- Equipment faults were often identified only after process interruptions occurred
- Reactive maintenance increased downtime and maintenance costs
- Limited visibility into pumps, blowers, motors, valves, and other critical equipment conditions
Treatment & Process Performance Challenges
- Delayed detection of abnormal water levels, aeration issues, membrane pressure variations, pump failures, and process deviations
- Difficult to continuously monitor critical treatment parameters and membrane performance
- Increased risk of filtration inefficiency, treatment disruptions, and reduced plant performance
Lack of Predictive Maintenance
- Maintenance was performed on fixed schedules instead of actual equipment and membrane condition
- Early signs of pump, blower, motor, valve, or membrane performance issues often went unnoticed
- Increased wear on critical equipment and higher maintenance costs
No Remote Monitoring & Instant Alerts
- Plant operators had to be physically present to inspect MBR process and equipment conditions
- Fault notifications and membrane-related alerts were delayed or unavailable
- Slow response to critical events increased operational downtime and affected treatment performance
Solution – AdiCloudX Industrial IoT Platform
AdiCloudX was deployed to transform the MBR sewage treatment plant into a smart, connected, and intelligent monitoring system. The solution enabled centralized monitoring of the MBR treatment process, water quality parameters, membrane filtration, pumps, blowers, motors, power consumption, and equipment health through a secure cloud-based SCADA platform.
Industrial data from PLCs, flow meters, level sensors, dissolved oxygen sensors, pH sensors, turbidity sensors, pumps, blowers, valves, motor controllers, energy meters, membrane systems, and other field devices is collected through the AdiNexus Industrial IoT Gateway and securely transmitted to the AdiCloudX cloud platform, where it is processed, analyzed, and visualized through real-time dashboards.
The platform continuously monitors MBR process status, tank levels, inlet and outlet flow, membrane filtration, transmembrane pressure (TMP), aeration, dissolved oxygen, pH, turbidity, pump and blower operation, motor health, valve status, power usage, alarms, and fault conditions. Automated alerts, historical trend analysis, equipment health monitoring, and remote access provide complete visibility into plant performance, helping reduce downtime, improve treatment efficiency, optimize maintenance, and enhance overall operational efficiency.
The system enables:
- Real-time MBR treatment process monitoring
- MBR process and filtration status tracking
- Tank level and inlet/outlet flow monitoring
- Membrane filtration and TMP monitoring
- Aeration and dissolved oxygen monitoring
- pH, turbidity, and critical process parameter monitoring
- Feed, circulation, permeate pump, blower, motor, and valve operation monitoring
- Power consumption and electrical parameter monitoring
- Equipment fault and alarm management
- Membrane performance and condition monitoring
- Equipment downtime and maintenance tracking
- Historical trend analysis and process performance reporting
- Proactive maintenance and equipment health monitoring
- Remote monitoring and centralized dashboard access
- Instant notifications for critical operational events
- Operational analytics and plant performance reporting
Why Choose AdiCloudX SCADA
AdiCloudX is a powerful Industrial IoT Cloud SCADA platform developed by AdiInfi, designed for MBR STP monitoring, wastewater treatment, industrial automation, and infrastructure management applications.
The platform enables organizations to digitally transform conventional sewage treatment plant operations into intelligent, connected, and data-driven systems with improved treatment efficiency, membrane performance, equipment reliability, operational visibility, and maintenance efficiency.
It enables facilities to
- Connect PLCs, Sensors, Pumps, Blowers, Membrane Systems, Flow Meters & Industrial Devices
- Real-Time MBR Process and Equipment Monitoring
- Membrane Performance & Equipment Health Analytics
- Reduce Equipment Downtime & Maintenance Costs
- Monitor and Optimize Energy Consumption
- Centralized Cloud SCADA Platform
- Historical Data Logging & Reporting
- Secure Industrial Communication
- Remote Monitoring & Mobile Accessibility
Scalability & Deployment
The platform is designed for high scalability and multi-site operations, allowing organizations to:
- Monitor multiple MBR treatment units from a single dashboard
- Manage multiple MBR STP and wastewater treatment plants across different locations
- Integrate geographically distributed treatment facilities
- Standardize monitoring and operational processes across all sites
Conclusion
With real-time dashboards, membrane and equipment analytics, automated monitoring, and centralized reporting, plant operators gained complete visibility into the MBR treatment process, membrane performance, equipment health, critical process parameters, and energy consumption across the entire sewage treatment plant.
The deployment significantly improved treatment plant reliability, reduced unexpected equipment downtime, optimized maintenance activities, improved membrane and process monitoring, and enabled faster decision-making through real-time operational intelligence.
This case study demonstrates how Industrial IoT and cloud SCADA platforms like AdiCloudX can modernize MBR STP operations through intelligent process monitoring, membrane performance analysis, equipment health monitoring, remote diagnostics, and data-driven operational insights.
Using AdiCloudX and the AdiNexus Industrial IoT Gateway, organizations can build scalable, reliable, and future-ready MBR STP monitoring systems that improve treatment efficiency, enhance membrane and equipment reliability, reduce maintenance costs, and maximize plant uptime.